Published: .
An inspector records two problems on one toothpaste tube, two on another and one on a third. Purchasing receives a message saying “five defective tubes.” The supplier receives photographs of three tubes. Before anyone can discuss the delivery, the teams need to resolve a basic counting error: five findings do not necessarily mean five affected units.
Toothpaste tube inspection defect counting needs a defined unit, a rule for recording findings and a clearly labelled denominator. This guide offers a fictional worked record for buyers reviewing inspection information. It does not choose an acceptance sampling plan, prescribe an AQL or declare a lot acceptable. The responsible quality parties must agree the applicable requirements and decision rules for the actual purchase.
Define the Unit Being Inspected
Tube Body or Complete Assembly?
For toothpaste tube packaging, state whether the inspected unit is a body, an assembled tube with its cap or another defined item. A cap supplied separately may have its own inspection record. Do not mix component counts with assembly counts without explaining the basis. The quotation and quality agreement should identify what purchasing expects to receive and what the inspection record covers.
Connect Each Observation to a Unit ID
Give the inspected specimens identifiers that let the reviewer connect findings, photographs and the physical items. An image filename alone may not show whether two photographs represent the same tube. Record the unit reference with each observation. The objective is to preserve identity so totals can be reconstructed without counting photographs as though they were separate products.
Distinguish a Finding from an Affected Unit
One Unit Can Have More Than One Issue
The ASQ quality glossary distinguishes a defect from a defective unit, which may contain one or more defects. In a purchase record, use the terminology agreed by the quality parties; “nonconformity” may be the relevant term for a failure to meet a specified requirement. The important counting distinction is between recorded issues and the unique units affected by them.
Establish the Requirement Before Confirming the Count
An observation is not automatically a confirmed nonconformity. Connect it to the applicable requirement, reference and review decision. If its status is unresolved, mark it pending rather than inserting it silently into a confirmed total. Keep the original observation available so the responsible quality reviewer can understand how the final classification was reached.
Keep Severity Rules Explicit
The counting basis and any severity categories are separate questions. Ask the quality parties how the applicable plan treats a unit with findings in more than one category. Do not invent a universal rule for combining categories, and do not assume that category totals can simply be added to produce the number of unique affected units. A traceable unit-level record makes the distinction visible.
Work Through a Fictional Inspection Record
Begin with Three Identified Tubes
The next table is an arithmetic and record-keeping exercise only. Imagine that 100 defined assemblies were inspected and that the listed observations were confirmed as separate nonconformities under the exercise’s assumed requirements. The remaining 97 assemblies have no recorded nonconformity in this fictional record. The quantity of 100 is not a recommended sample size or a Xinfly inspection result.
| Unit ID | Recorded requirement categories not met | Number of confirmed nonconformities | Counts as one affected assembly? |
|---|---|---|---|
| U001 | A and B | 2 | Yes |
| U002 | A and C | 2 | Yes |
| U003 | B | 1 | Yes |
| Other 97 assemblies | None recorded in this exercise | 0 | No |
| Total | A occurs twice; B twice; C once | 5 | 3 affected assemblies |
The letters A, B and C are fictional category labels. They do not define actual toothpaste tube defects or severity classes. In a real record, replace them with agreed requirement references and the responsible reviewer’s decisions. Do not infer from the example that every visible mark, colour difference or component observation should be classified in the same way.
Calculate Two Different Metrics
In this exercise, the observed proportion of affected assemblies is 3 ÷ 100 = 3%. The nonconformity count per inspected assembly is 5 ÷ 100 = 0.05. Expressed per 100 inspected assemblies, that second metric is 5 nonconformities per 100 assemblies. These metrics describe different quantities. Five nonconformities must not be relabelled as five affected assemblies or an observed 5% affected-unit rate.
Keep the Result Within the Observed Record
The arithmetic describes the fictional inspected group. It does not establish a production lot’s true quality or decide whether a shipment should be accepted. Avoid turning a sample observation into an unsupported statement about every tube in the delivery. Any lot decision must use the applicable agreed plan, its counting basis and the authorised quality review.
Keep the Denominator with Every Total
Identify Which Units Were Checked for Which Requirement
A report may include different checks performed on different groups or at different stages. Record the inspected quantity relevant to each result. Do not divide a count from one group by the quantity from another because it produces a convenient common percentage. Ask the reviewer to explain any difference in scope before purchasing compares the figures.
For laminated toothpaste tube packaging, identify the structure and inspection stage along with the item reference. An empty incoming assembly, a filled specimen and a pack after another evaluation may belong to different records. This guide does not define their test conditions or combine their results. Keep the evidence for each stated question separate and traceable.
Count Unique Affected Units Only Once in an Overall Total
When the overall metric concerns units affected by at least one of the reviewed nonconformities, count distinct unit IDs. In the example, A involves U001 and U002, while B involves U001 and U003. Adding those two category counts gives four occurrences, but the union of their unit IDs contains three assemblies. Preserve that relationship rather than hiding it in an unlabeled total.
Do Not Apply a Sampling Decision to the Wrong Count
Read the Plan’s Counting Basis
NIST’s single sampling plan explanation describes a plan using a sample size and an acceptance number based on defective units. It illustrates why the quantity counted must match the plan’s definition. It does not establish a sampling plan for your tube order. Ask the responsible quality parties to identify the applicable plan and explain its use.
Keep the Acceptance Decision Separate from the Worksheet
A worksheet can organise observations and calculate totals correctly without establishing acceptability. The project’s quality assurance review should connect the requirements, sampling approach, classification rules and decision authority. Do not insert an acceptance number from another project or treat a familiar AQL label as permission to choose whichever count gives a preferred outcome.
Make the Evidence Useful to the Supplier
Retain the Unit-Level Links
For each confirmed issue, keep the relevant unit ID, location, requirement reference, image and reviewer’s decision. Include an overall view when a close-up alone does not identify the specimen or location. Ask the supplier which additional information is needed for its investigation. Several images of one issue should remain linked to that issue rather than multiplying the count.
Separate Observation, Classification and Cause
An inspector can record what was seen. The authorised reviewer can determine its status against the requirement. An investigation may then address cause. Keep those stages distinct. A confirmed nonconformity count does not automatically establish why it happened, which process caused it or which commercial remedy applies. Avoid adding an unsupported explanation to otherwise useful evidence.
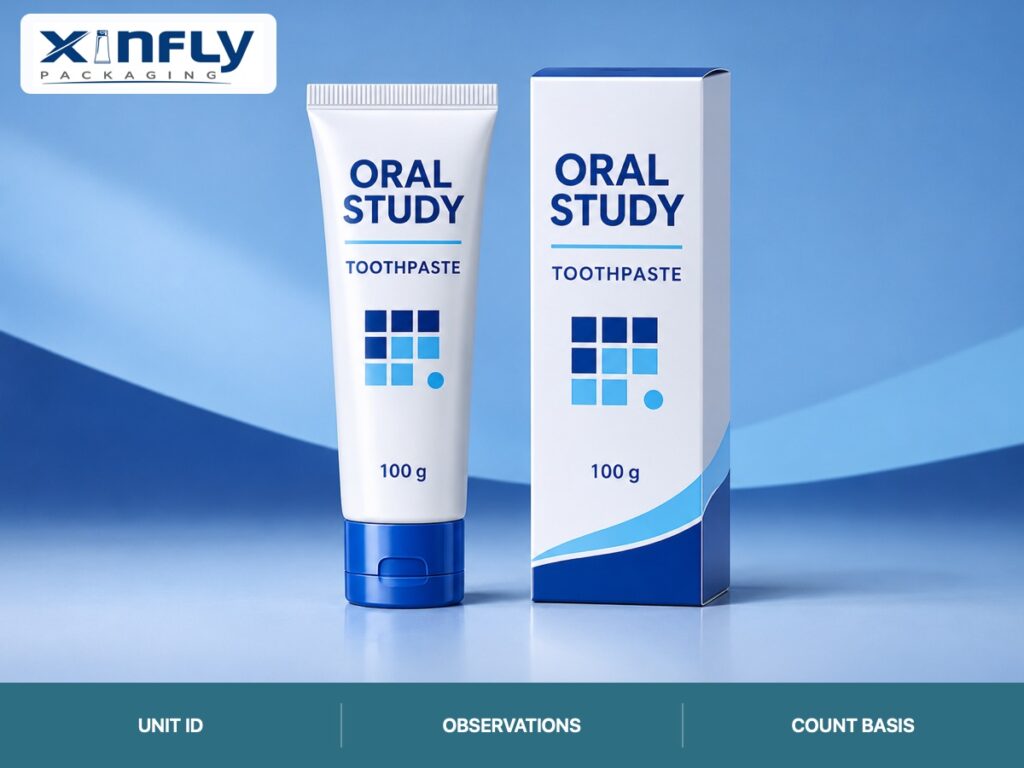
The illustrations use a fictional ORAL STUDY pack: an opaque white PBL-style body, moulded shoulder, straight crimped display tail and cobalt round stand-up flip-top cap. Navy and sky-blue offset-print-style wording, grid and circle coordinate with its printed carton. The illustrated pack is clean and undamaged. It does not show actual inspection findings or represent the fictional U001–U003 specimens.
Use a Summary That Can Be Reconstructed
| Field | What to retain | Question it resolves |
|---|---|---|
| Purchase item | Body, closure and applicable revisions | Which configuration was inspected? |
| Lot and scope | Relevant lot reference and inspection stage | Which material does the record concern? |
| Unit definition | Body, assembly or other agreed item | What does one inspected unit mean? |
| Inspected quantity | Quantity relevant to the stated checks | What is the denominator? |
| Confirmed findings | Requirement, unit ID and classification | What issues are included in the count? |
| Unique affected units | Distinct unit IDs under the stated rule | How many units are affected? |
| Pending observations | Unresolved status and reviewer | What has not yet entered the confirmed total? |
| Decision basis | Agreed plan, scope and authority | Who can make the applicable lot decision? |
This summary supports review. It does not specify a sampling method, sample quantity or acceptance threshold. The underlying unit-level record should explain how each total was produced. If the inspector, supplier and buyer cannot reconstruct the same total, resolve that discrepancy before relying on the summary for a purchasing or disposition decision.
Clarify the Count Before Discussing the Outcome
A practical message can read: “Please confirm whether the reported figure counts confirmed nonconformities or unique affected units. Identify the inspected unit, relevant inspected quantity and requirement categories. Please connect each finding and image to a unit ID, show pending observations separately, and identify the agreed plan and reviewer responsible for any lot decision.” Attach the original report so the clarification has a specific reference.
When buying empty toothpaste tubes wholesale, agree the relevant quality documentation before the order reaches receiving. Use sample development to establish representative references for the questions the project needs reviewed. Do not turn an appearance sample into an unrecorded defect standard. Keep the approved reference, applicable requirements and counting definitions available to the people who will inspect the delivery.
Frequently Asked Questions
Can one toothpaste tube have several recorded defects?
Yes, a defined unit can contain more than one issue under the relevant requirements. Record each finding against the same unit ID. When calculating an overall affected-unit total, use the applicable unique-unit rule rather than automatically counting each finding as a separate tube.
Are five findings in 100 tubes always a 5% defective rate?
No. You need the number of unique affected tubes to calculate an observed affected-unit proportion. In the fictional example, five nonconformities occur on three of 100 assemblies, giving a 3% observed affected-unit proportion. The issue-count metric remains separately labelled.
Can I add counts from different defect categories?
You can calculate a stated issue-count total where the rules support it, but that may not equal the number of unique affected units. Categories can involve the same unit. Keep unit IDs and the applicable classification rules available before combining or interpreting category totals.
Does a correct count establish whether the lot passes?
No. The applicable agreed sampling plan, requirements and decision authority are also needed. This article provides no acceptance number or universal AQL. Ask the responsible quality parties to make and document the lot decision using the correct counting basis.
What should I send Xinfly Packaging with a concern?
Send the purchase and lot references, inspected-unit definition, relevant inspected quantity, unit-level observations, images and applicable requirements. Distinguish confirmed findings from pending questions. Ask Xinfly Packaging to review the traceable record and identify any further information needed.
Conclusion: Count the Issues and the Units Separately
A useful inspection record preserves the connection between each finding, its physical unit and the relevant requirement. Clear denominators and labelled metrics let the buyer and supplier discuss the same evidence. Contact Xinfly Packaging with your toothpaste tube specifications and quality-documentation needs to establish the appropriate references before ordering.