Published: .
Technical review: pending.
Laminate tube roll change traceability tells the buyer which finished tubes came from each printed material run. Two adjacent rolls may carry the same brand design and their finished tubes can look similar. If a later question concerns a color revision, an unidentified input roll or a carton at the line transition, appearance alone gives the buyer little to work with. Before issuing the purchase order, agree how the converter records both sides of a roll change and how those records connect to retained tubes and identified cartons.
Confirm Where the Roll Enters the Process
Define the Quote Scope
Ask the converter whether it will feed printed rollstock to form the tube bodies, print during a separate step or decorate already formed tubes. This guide follows a job where a printed laminate roll is used in body converting. If the supplier prints on formed tubes, keep the material roll record and the decoration record as two related references. Note which operation creates each identifier and which team can verify it. Get the process route in writing so quotes covering different stages can be compared.
Name the Body, Decoration and Assembly
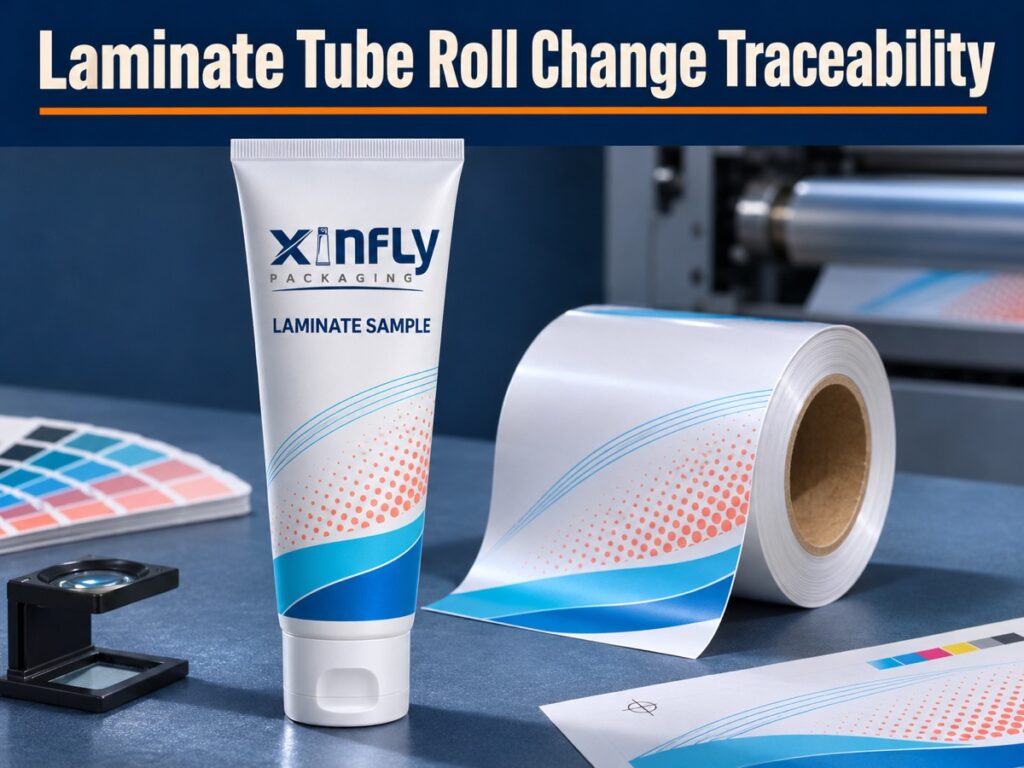
The proposal illustrated here is a white round PBL body with a formed side seam, molded shoulder, broad white closed flip-top cap and a straight heat-sealed tail on the finished reference. The printed reference uses a blue and coral layered offset motif. Ask for the agreed laminate construction and decoration method in the assembly drawing and quote. Use the same finished tube configuration for all retained samples. A change to the cap or shoulder revision may need a separate record even when the body artwork stays the same. The product collection describes options for plastic barrier laminate tubes.
Link the Roll to the Samples
Build a record that connects the input roll label, the job and artwork revision, the first and last relevant finished tube references, and a carton or other output range. Decide how the parties will identify samples upstream and downstream of the changeover. For example, an internal record may call one illustrative roll A and the next roll B. The production record needs an identifier suitable for the supplier's own system. Show the full identifier on the retained records rather than expecting someone to distinguish the rolls by artwork alone.
Capture the Outgoing and Incoming Sides
Ask the converter to retain the last agreed group from the outgoing roll and the first agreed group from the following roll. Request a roll label record on each side and define how the retained samples will be physically identified. Confirm whether the converter can associate the finished cartons with an actual boundary in sequence. If units can accumulate between operations, ask where that accumulation occurs and how the affected range will be held or segregated.
| Field | Outgoing roll | Incoming roll | What the buyer should be able to verify |
|---|---|---|---|
| Roll identity | Full label record and last run timestamp or sequence | Full label record and first run timestamp or sequence | Both identifiers are distinguishable and linked to the same job |
| Material and artwork | Construction and decoration revision in use | Construction and decoration revision selected next | Whether the conversion continued with the approved revisions |
| Finished references | Identified retained tube and optional print strip | Identified retained tube and optional print strip | Each reference has a clear place on one side of the change |
| Output range | Last identified carton, tray or lot before the transition | First identified carton, tray or lot after it | The buyer knows which records to consult in a later investigation |
| Uncertain output | Containers or quantities held pending identification | Release decision and the person who made it | Whether any unit from the transition could have mixed into available stock |
| Sign-off | Job, line and operator record | Reviewer, decision and confirmation time | The record can be retrieved with the purchase order |
Keep Sample Identity Independent of Appearance
Label each retained tube in a way that does not obscure the print field or seam to be inspected. Use a separate tag or retained sample bag if the label itself could change the appearance. Confirm the label connects to the conversion job and the appropriate roll ID, not just an internal item number printed on every carton. If the supplier keeps a separate film strip, record which roll it represents and how it was obtained. Use the laminate tube construction guide for context when identifying the actual tube structure named in the samples.
Review the Changeover Pack
Ask for the linked records as a small packet that someone outside the shop can read. It can contain electronic files, photographs and a sample register. Ask an employee who did not collect the record to start with one carton identifier and find its corresponding roll and retained tube reference, where that information is available. Then start from the incoming roll and look for the output range related to it. Discuss any ambiguity with the converter while the shop records are still available.
Define When to Hold Finished Tubes
Before ordering, agree which changes require review or line clearance. Typical triggers to discuss include a change to the approved artwork revision, a label discrepancy and an uncertain output range. When a transition falls within a carton, ask how that carton will be identified or segregated. If the converter cannot recover a unit-level distinction, the buyer and converter need to define the affected carton or lot range and record the disposition. Keep this decision visible on the release record.
| Situation in the record | Suggested procurement disposition | Evidence to request before release |
|---|---|---|
| Different roll IDs and same released construction and artwork | Review both retained references under the agreed scope | Linked roll labels, first and last references and the carton mapping |
| New artwork revision planned | Keep the new revision on hold until the project approval is confirmed | Approved revision, transition checks and separate identification in the first released output |
| Roll label incomplete or not matched | Hold the affected range and establish traceability with the converter | Original label or approved reconciliation and responsible reviewer |
| Output between the two rolls uncertain | Define a conservative hold range with the responsible team | Held carton IDs, recovered links if available and documented disposition |
| Sample looks right but the recorded roll differs | Reconcile the identity of the sample before using its approval | Verified sample ID, drawing and a corrected record with reviewer sign-off |
Ask a Quote Question About the Real Boundary
A supplier may be able to map output to cartons but lack an identifier on individual loose tubes. If your project needs greater detail, ask suppliers to state which traceable unit their records support and what would be required to go further. Compare a carton-level proposal with a lot-level one using the work your team would face after a receipt concern. Include repack handling at the filler if its teams split or combine cartons. Retain container identifiers during any repack where the buyer requires them.
Document the Request in the Purchase File
Send the converter the tube assembly and graphics revisions, the permitted ranges for each output identifier and the retained sample method. Ask the supplier to describe who checks roll identity and who authorizes release at the change. Name the records to be supplied with the first production trial and the retention period to agree for repeat orders. For laminated cosmetic tubes with different language versions, request the exact version on each retained tube record so that a similar front panel cannot stand in for version identification.
Set the Audit Exercise Before Production
Use a Representative Example
During the first review, ask the converter to demonstrate the process with a clearly labeled trial, preferably using the project route. Choose an outgoing and incoming sample and one finished output range. Verify the link back from the sample to the job and compare the defined record with what would reach the filler. If the exercise reveals a missing transfer, revise the handoff before approving the first production record. This is an identity and traceability check for the stated configuration. Use separate evidence when deciding performance, materials or printing acceptance.
Walk Through an Uncertain Carton
Imagine the record shows that roll A finished before a change to roll B but some tubes from the transition reached a single identified tray between forming and pack-out. The tray can be traced to two finished cartons and the individual units were never marked with a roll identity. In this example, ask that both cartons stay on hold while the converter checks the intermediate tray record. Capture the carton IDs, who investigated and whether the affected output can be defined further. If the result remains uncertain, agree a disposition for the carton range rather than treating the timing of the new roll as the unit boundary. Keep the paired retained samples accessible with the related paperwork. A new print or material approval would require its own evidence. This example illustrates the purpose of recording an intermediate container as well as the finished carton.
Frequently Asked Questions
Do all laminated tubes use printed rollstock?
Ask the converter how your particular body will be made and decorated. If it prints after forming, identify the material roll in the forming record and the graphics revision in the decorating record. Match both to the finished sample before comparing production runs.
How should I record a change to a new roll of the same artwork?
Capture both roll identifiers, their shared artwork revision, the relevant finished references and the output range under the agreed plan. The records should let the buyer locate the same evidence later without depending on a visible difference.
Can I identify the roll solely from the finished tube?
Only where the supplier has explicitly agreed an identifier or reliable mapping for your project. Ask what the buyer can trace once units leave the original packaging. Confirm that any buyer or filler repack keeps the references needed for the agreed scope.
Can a good roll change record stand in for print quality approval?
Use the record to identify which inputs and output are related. Approve print on the relevant physical references according to the separate project criteria. If you change the artwork or print route, ask what additional check should be completed on the next run.
What should I include in an RFQ for laminated tube packaging?
Provide the laminate construction, assembly, cap and artwork revisions, and explain the unit of traceability you need. Ask the supplier to quote the retained samples and output mapping for the first trial, note any exceptions and name the owner of the release record.
Conclusion
Require a clear link between input roll identification, the approved artwork, retained tubes and finished cartons. Test the handoff before ordering and document which output must be held if the record leaves a gap. Send Xinfly Packaging your draft record, proposed body and artwork when you request a laminated tube production sample quote so the proposed converting route, samples and traceability can be discussed together.