Published: .
Your toothpaste tube supplier sends a cap torque figure. The filler sends another. One is written in N·m and the other in N·cm, with no explanation of when or how the measurement was made. A number that appears much larger may represent exactly the same torque, while two matching numbers may describe different tests.
A toothpaste tube cap torque specification units check starts with both the unit and the measured action. Begin with the proposed toothpaste tube packaging, then identify the threaded closure or threaded base involved. This guide provides conversion examples and an RFQ record. It does not set a capping-machine adjustment or an acceptable torque range for any tube.
Identify the Closure Action Before Comparing Numbers
Separate Threaded Assembly from Flip-Lid Opening
A flip-top closure can involve a lid-opening action and, depending on its design, a separate threaded attachment to the neck. Identify which action the specification describes. Do not assume that a figure for opening the lid tells you the torque used to apply or remove a threaded closure assembly. Confirm the actual design on the drawing.
For custom toothpaste tubes with stand-up caps, send the complete cap and neck references together. The stand-up description concerns the pack configuration, not a universal thread or test method. If the proposed attachment is not threaded, ask which measurement and acceptance description are relevant rather than forcing it into a threaded-cap torque worksheet.
Name Application and Removal Measurements Separately
Application refers to the closing operation described by the agreed method. Removal concerns the opening measurement under its stated conditions. They are different observations, so keep their labels distinct. A removal reading should not be copied into a machine-setting field simply because both are reported in the same torque unit.
Ask the supplier and filler what each reported value represents. If terms such as initial opening, peak or another reported measure are used, request the method’s definition. Avoid treating an instrument’s displayed number as self-explanatory when the project record does not identify the action, sample or reporting convention behind it.
Normalize Torque Units on the Comparison Sheet
Read the Prefix and the Separator Carefully
Torque is expressed using a force multiplied by a distance. NIST’s SI units reference identifies the newton meter as the SI unit for torque. A newton centimeter and a millinewton meter use different prefixes. Keep capitalization and the multiplication relationship clear when copying units from a quotation or instrument record.
The NIST SI prefix reference gives centi as one-hundredth and milli as one-thousandth. Consequently, 1 N·m equals 100 N·cm or 1,000 mN·m. The conversion changes the number used to express the torque; it does not change the underlying torque or make unlike measurement methods equivalent.
Do Not Treat N/mm as Another Spelling of Torque
A slash and a multiplication mark communicate different relationships. If a supplier writes an unclear unit, ask for confirmation rather than silently correcting it. Likewise, N·mm and mN·m both represent torque units, but their symbols describe different prefixed factors. Record the source notation and your confirmed conversion so the comparison can be checked later.
| Hypothetical torque in N·m | Same torque in N·cm | Same torque in mN·m | Same torque in N·mm |
|---|---|---|---|
| 0.15 | 15 | 150 | 150 |
| 0.20 | 20 | 200 | 200 |
| 0.30 | 30 | 300 | 300 |
These values are invented arithmetic examples. They are not Xinfly cap specifications, test results, suggested trial limits or filler settings. For example, 20 N·cm and 0.20 N·m describe the same torque. They still cannot be compared as equivalent test results unless the measured action, assembly and conditions are meaningfully aligned.
Put the Measurement Stage Beside the Unit
Identify the Actual Sample State
Record whether the sample is an empty component assembly, a filled pack or another defined state. Identify prior opening or closing where it matters to the agreed method. A newly assembled cap and a previously handled sample should not be described as the same condition merely because their product names match.
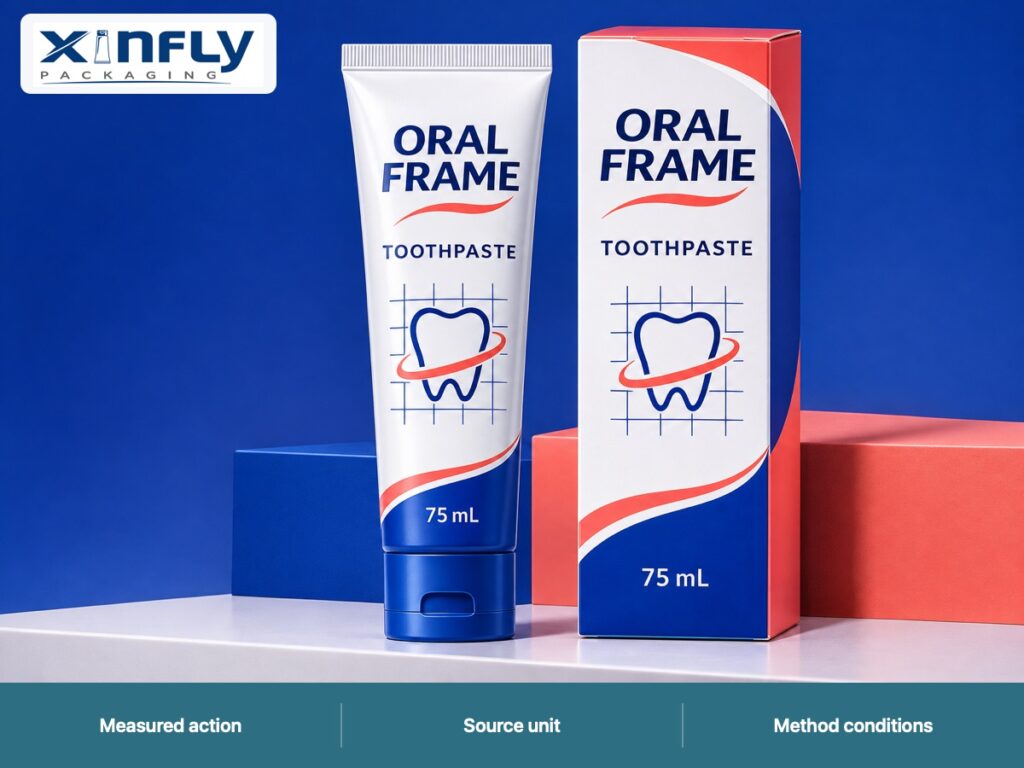
The ORAL FRAME illustrations show a nominal 75 mL white PBL body, molded shoulder, straight sealed display tail, cobalt flip-top and navy, cobalt and coral offset artwork. The printed carton repeats the design. The pictures do not establish a thread specification, an attachment method or any torque result. The actual cap-and-neck arrangement needs its identified drawing.
Record the Relevant Interval and Conditioning
Ask the responsible teams which interval after application and which preparation or storage conditions belong in the method. Keep the actual conditions with the result. Do not compare a reading taken at one defined stage with another taken after a different history and attribute the difference only to supplier quality.
This guide does not prescribe a waiting period, conditioning temperature or operating speed. Those decisions depend on the assembly, purpose and selected method. If a report omits them, mark the omission and request the information needed for the actual comparison instead of inventing a convenient default.
Keep the Instrument and Fixture Part of the Record
Define How the Pack Is Held and Operated
Ask the testing owner to describe the relevant instrument, holding arrangement and operation under the chosen method. The worksheet should make clear what is measured and how the tube and cap are presented. A photograph of a hand tool beside a tube is not a substitute for an identified test setup or an instrument record.
Where instrument status, calibration or verification matters to the project method, retain the actual supporting record. Do not describe a measurement as traceable or certified without the applicable evidence. Purchasing can ask which records are available and whether they support the intended acceptance decision; it should not infer those attributes from a device’s appearance.
Preserve Raw Results and Source Units
Keep the original result and source unit alongside the normalized value used for comparison. Record the conversion factor rather than replacing the source number with an unexplained new number. If results for several samples are summarized, retain the individual records and the stated summary approach so unusual observations remain visible.
Do not turn missing readings into zeros or hide an unclear unit behind an average. A zero is a measurement value with a particular meaning in the method, while an unavailable result is a different status. The responsible quality owner should define how incomplete records affect the acceptance decision.
Convert Both Ends of a Reported Range
If the source gives a range, retain and convert both endpoints. For an arithmetic example only, 0.18–0.22 N·m becomes 18–22 N·cm or 180–220 mN·m. Copying only the midpoint loses information about the range the source actually reported. These example endpoints are not proposed acceptance limits for the illustrated pack or any other closure.
Keep the reported precision visible too. A conversion can change the placement of the decimal point without improving the original measurement. Avoid adding extra digits that imply evidence the source record does not contain. If rounding is needed for a comparison sheet, retain the unrounded source value and agree the reporting approach with the responsible measurement owner.
For a spreadsheet handoff, put the source number and unit in separate fields, then identify the conversion factor and normalized result. Keep application and removal records in separate labeled rows. That arrangement lets another buyer check the calculation and the measurement meaning without guessing which action a single column headed “cap torque” was meant to represent.
Make the RFQ Ask for a Complete Specification
Separate a Proposed Setting from an Acceptance Result
A machine setting is an operating input. A result measured on the assembled sample is an observation under a method. Ask the filler and packaging owner how they relate within the project’s qualification plan. Do not assume they are interchangeable or that a nominal machine display alone establishes the finished assembly’s acceptance.
For laminated toothpaste tubes, preserve the agreed body, shoulder or head and closure references while reviewing the capping proposal. If a supplier changes a relevant component, ask which measurements or process checks need reassessment. A shared nominal capacity or similar cap color cannot establish equivalence of the mating parts.
| Record field | Supplier or testing-owner response needed | Purpose for the buyer |
|---|---|---|
| Assembly | Tube head or neck and closure references, including revisions | Identifies the parts involved |
| Measured action | Application, removal or another explicitly defined observation | Prevents different actions being compared |
| Unit | Full source notation and confirmed normalized unit | Prevents a prefix or transcription error |
| Sample state | Empty or filled, preparation and relevant prior handling | Makes sample histories distinguishable |
| Method conditions | Relevant interval, conditioning and operating procedure | Defines what the result represents |
| Instrument and fixture | Applicable setup and supporting status records | Connects the result to its measurement basis |
| Acceptance criteria | Project-approved limits, method and responsible owner | Keeps arithmetic separate from qualification |
| Order scope | Released references and affected supply | Makes the approval usable for purchasing |
Keep Torque Separate from Other Package Requirements
Do Not Use One Result to Claim Complete Pack Performance
A torque result does not, by itself, establish leakage performance, shipping suitability, repeated-use behavior or formula compatibility. Identify which additional checks the project requires and keep their evidence separately traceable. A cap that meets one defined criterion has not automatically passed every requirement for the toothpaste pack.
Xinfly Packaging’s caps and closures information can support the component discussion, while its quality assurance information provides context for agreeing project checks. Use those resources to formulate the required records. The actual acceptance plan should identify the relevant assembly, methods and criteria rather than treating a webpage as a universal test standard.
Send Xinfly Packaging a Comparison-Ready Brief
Include the Unit Problem and the Intended Decision
Provide the assembly references, formula information needed for review, supplied state, intended filling route and the specific result or setting that needs clarification. Attach the original notation, even if it appears inconsistent. Asking the supplier to confirm the source meaning is more reliable than forwarding only a converted number without its context.
Use sample development to discuss which sample states and responsibilities the project needs. Send Xinfly Packaging your closure specification question with the filler’s requirements and intended order scope. Confirm actual sample availability, costs, quantities and timing for the proposal rather than borrowing assumptions from another tube project.
Frequently Asked Questions
Are 20 N·cm and 0.20 N·m different torque values?
They express the same torque. The numerical values differ because the distance unit differs. Matching the torque value does not establish that two tests are comparable; confirm the measured action, assembly and conditions as well.
Can a removal reading be used directly as the capping-machine setting?
Do not assume that relationship. A setting and a measured removal result describe different stages. Ask the responsible process and packaging teams to define the method and qualification basis for the actual assembly.
Does opening a flip-top lid measure the threaded attachment torque?
Not automatically. Identify which part moves and what the method measures. If the closure has a threaded base, its attachment or removal is a separate action from opening the hinged lid. Confirm the actual construction on the drawing.
What should I do when a quotation gives an unclear unit?
Keep the original notation and request clarification from the source. Do not silently assume the intended unit, particularly when capitalization, prefixes or a slash could change the meaning. Retain the confirmed conversion with the quotation record.
What should a repeat order reference?
Use the released mating-part references, relevant material and process scope, measurement method and project acceptance criteria. Identify any proposed change before supply. Keep the historical results tied to their actual sample and test conditions.
Conclusion
A useful cap torque specification identifies the action, unit, assembly and method together. Normalize the arithmetic, preserve the source result and keep settings separate from measured acceptance evidence. That gives Xinfly Packaging, your filler and your buying team a practical way to compare toothpaste tube closure information without mistaking a unit conversion for a technical approval.